+91 98209 33660
Engineered for continuous OEM duty, high mechanical efficiency, and seamless NEMA frame integration across American industrial plants.
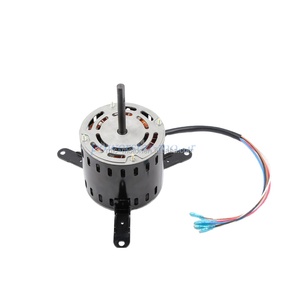
Compact 60Hz US voltage motor optimized for precision gear reduction assemblies, fluid pumps, and air handling equipment.
Inquire Now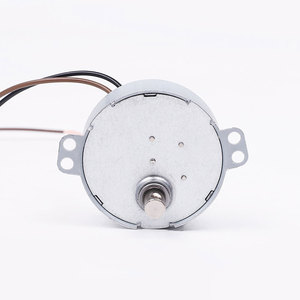
Micro-helical precision reduction gearhead engineered for exact speed control, low RPM HVAC dampers, and automation actuators.
Inquire Now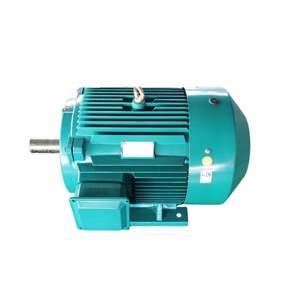
Premium efficiency pure copper core motor designed for direct coupling with high-horsepower industrial helical gear reducers.
Inquire Now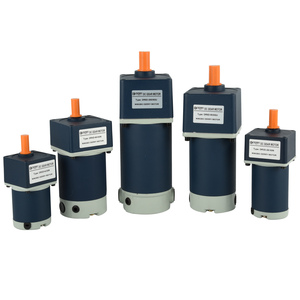
Scalable 6W to 750W 110V/220V continuous-duty gear motor with hardened alloy helical gears for commercial conveyors.
Inquire Now
High-efficiency single & three-phase AC motor optimized for heavy machinery, hydraulic power packs, and reducer mounting.
Inquire Now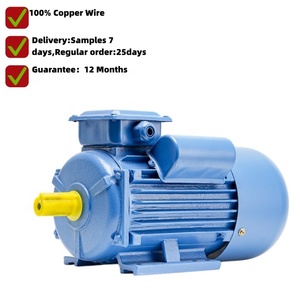
High starting torque single-phase drive engineered to power farm equipment, commercial mixers, and rugged helical gearboxes.
Inquire Now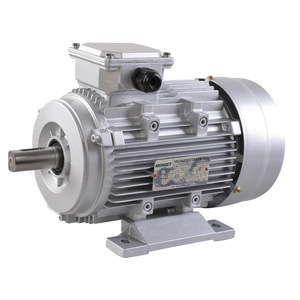
Lightweight thermal-dissipating alloy housing combined with 4-major series helical gear reducer frames for US OEM machinery.
Inquire Now
Ultra-quiet, precision-ground gear train engineered for 24/7 continuous duty in automated dosing and valve positioners.
Inquire NowIn modern North American manufacturing, power transmission efficiency, thermal dissipation, and structural reliability dictate overall operational profitability. As plant managers and OEM design engineers across the United States replace legacy right-angle worm gearboxes with high-efficiency inline helical, helical-bevel, and parallel shaft helical gear reducers, understanding the underlying gear tribology, tooth contact mechanics, and AGMA (American Gear Manufacturers Association) load factors becomes essential.
Key Engineering Advantage: Unlike standard worm drives that lose up to 30–40% of input electrical energy to sliding friction, precision helical gear sets operate via rolling contact, delivering mechanical efficiencies between 95% and 98.5% per reduction stage. Over a 5-year operating lifecycle in a US continuous-duty plant, this reduction in energy losses translates directly to thousands of dollars in lower utility costs and decreased HVAC cooling loads.
The performance foundation of our export-grade helical gearboxes relies on advanced tooth modification and metallurgical discipline. Gear sets are forged from premium 20CrMnTi / AISI 86ize low-alloy steel, undergoing vacuum carburizing and oil quenching to achieve a surface hardness of 58–62 HRC while maintaining a tough, shock-absorbent core (30–40 HRC).
Properly sizing a helical gearbox for the US market requires calculating the required Service Factor (SF) based on daily operating hours, ambient thermal conditions, and the shock characteristics of the driven load. The formula for required mechanical power ($P_{req}$) is:
$P_{req} = P_{absorbed} \times SF_{load} \times SF_{ambient} \times SF_{duty}$
| Application Load Type | Typical US Machinery Examples | Moderate Duty (8h/day) | Continuous Duty (16-24h/day) | Heavy Shock Load |
|---|---|---|---|---|
| Uniform Load (U) | Centrifugal Blowers, Uniform Conveyors, Clean Water Pumps | SF = 1.00 | SF = 1.25 | SF = 1.50 |
| Moderate Shock (M) | Food Mixers, Overhead Cranes, Reciprocating Compressors | SF = 1.25 | SF = 1.50 | SF = 1.75 |
| Heavy Shock (H) | Rock Crushers, Shredders, Extruders, Mining Mills | SF = 1.75 | SF = 2.00 | SF = 2.25 – 2.50+ |
Selecting the appropriate gearbox architecture depends on plant spatial constraints, mounting orientation, and shaft alignment requirements:
Tailored power transmission solutions engineered to withstand demanding operating environments across American manufacturing hubs.
In major logistics corridors such as the Inland Empire (California), Dallas-Fort Worth, and the Ohio Valley, distribution centers rely on continuous parcel sorting conveyors. Our R-Series inline helical geared motors deliver smooth start-stop operation with NEMA 56C/145TC motor flanges, keeping maintenance downtime near zero during peak holiday sorting windows.
For meat processing facilities in Wisconsin and Midwest dairy plants, sanitation is paramount. We export custom helical gear reducers featuring food-grade synthetic lubricant (USDA H1), double-lip vitreous fluoroelastomer seals, and antimicrobial coated aluminum/cast-iron housings that withstand daily high-pressure chemical washdowns.
Serving municipal engineering projects in Texas, Florida, and the Pacific Northwest, our K-Series heavy-duty helical bevel drives power thickener scrapers and aeration basins. Designed with reinforced output bearings to absorb heavy radial and axial shaft thrust loads without oil leakage.
Custom-wound 60Hz single and three-phase motors paired with low-vibration helical gear trains provide uninterrupted air delivery in commercial chillers and data center cooling towers throughout the Sun Belt region, operating seamlessly across ambient temperatures exceeding 115°F (46°C).
In Appalachian mining operations and Western aggregate processing facilities, heavy shock loads can cause premature tooth pitting. Our cast-iron FC250/GG25 housing helical gearboxes offer high torsional rigidity, resisting housing deformation under maximum mechanical overload.
Combining fractional horsepower synchronous AC motors with high-ratio precision helical gearheads allows chemical plants in Houston and Louisiana to achieve highly repeatable micro-metering without pulsation or speed drift.
How North American OEMs are modernizing drives to meet stricter energy standards and smart factory requirements.
With US Department of Energy (DOE) regulations strictly enforcing motor efficiency compliance, industrial buyers can no longer afford energy-wasting drive combinations. Paired with high-efficiency IE3/IE4 AC induction motors, our helical gearboxes help plants meet mandatory sustainability goals while slashing lifecycle electricity consumption.
US plant engineers are aggressively retrofitting old right-angle worm gear reducers with helical-bevel (K-Series) and parallel shaft (F-Series) drives. The shift from ~65% thermal efficiency to >95% helical efficiency yields an immediate return on investment (ROI) within 8 to 14 months of continuous operation.
Modern US smart factories demand real-time telemetry. Our export gearboxes can be pre-machined with threaded ports (1/4"-18 NPT or M8) to accommodate industrial accelerometers and RTD thermal sensors, allowing plant maintenance teams to monitor vibration spectrums and bearing temperatures before failures occur.
Uncertain domestic supply chains have pushed US equipment builders to establish direct relationships with reliable global gear manufacturers. By offering custom shaft modifications, ANSI keyways, and direct factory-to-port export logistics, we provide American OEMs with stable lead times and predictable component pricing.
Founded in 1974, our manufacturing facility brings over five decades of engineering discipline, state-of-the-art gear grinding technology, and stringent quality control to every unit shipped across the Atlantic.
Established shop-floor expertise in motor winding, gear cutting, heat treatment, and dynamic balancing guarantees long service life under harsh duty cycles.
From gear blank forging to final acoustic noise chamber inspection, every gearbox is 100% routine-tested for back-lash tolerance, thermal rise, and oil seal integrity.
Exclusively cut keyways to ANSI B17.1 specs and offer standard NEMA C-face input flanges (56C, 143TC, 184TC, 215TC, 256TC) for plug-and-play installation with American motors.
Heavy-duty vacuum-sealed rust-inhibiting VCI barrier foil wrapped in IPPC heat-treated wooden crates prevents salt-fog corrosion during sea transit to US ports (LA, Houston, Newark, Savannah).
Clear, direct technical answers regarding standards compliance, replacement interchangeability, and shipping logistics.
Submit your application parameters—required output torque, speed ratio, motor horsepower, and shaft orientation—and our application engineers will provide a verified CAD model and commercial quote within 24 hours.